Quick answer
Production fabrication is the repeat manufacture of welded parts and assemblies, such as equipment skids, machine frames, guards, brackets and wear parts, built to a customer drawing. We review the drawing for manufacturability, build fixtures to hold tolerances, run a first article for approval and then repeat the part with documented procedures and inspection.
Key points
Built to your drawing, revision-controlled from quote to delivery
Fixtures and weld sequences that control distortion and repeatability
First-article inspection and approval before the run
Process selection matched to material, joint and volume
Packaging, labeling and documentation to your requirements
What production fabrication means for industrial buyers
Production fabrication sits between a one-off custom build and high-volume stamping. Typical runs range from a handful of identical skids to recurring orders for hundreds of brackets, guards or frames. Buyers include equipment manufacturers, systems integrators, packaging and conveyor builders, energy equipment suppliers and fabrication shops that need overflow capacity.
The value is consistency. The tenth part should fit and perform exactly like the first, and the reorder six months later should match both. That outcome comes from process control, not from skilled welders working from memory.
Pump, compressor and process equipment skids
Machine bases, frames and weldments
Equipment guards, enclosures and access panels
Brackets, mounts, clips and support steel
Wear parts, liners and replaceable chute sections
Trailer-mounted and portable equipment frames
From drawing to approved first article
Every job starts with a drawing review. We look at tolerances, weld symbols, material callouts, finish requirements and inspection notes, and we flag anything that will be expensive or difficult to hold. A tolerance tighter than the function requires or a weld that cannot be reached with a torch is far cheaper to fix on paper than in production.
Once the drawing is agreed, we build a first article. It is inspected dimensionally against the drawing, with critical features measured and recorded, and sent to you or reviewed at our shop for approval. Only after approval do we release the run, and the approved revision is the one we build to until you issue a change.
Revision control matters on repeat work. Each order references a drawing number and revision, and superseded prints are pulled from the floor so an old version cannot slip into a new batch.
Fixtures, jigs and distortion control
Welding shrinks metal. Each bead pulls the joint as it cools, and on a long frame or a thin enclosure those small movements add up to warped parts that do not fit. Fixtures hold parts in position during tacking and welding, and a planned weld sequence balances the shrinkage so the finished part stays within tolerance.
For repeat runs, a purpose-built fixture pays for itself quickly. It locates every component the same way every time, reduces measurement and fit-up time, and makes quality less dependent on the individual fitter. For short runs, modular fixturing on a flat welding table often gives most of the benefit at lower cost.
Where distortion still occurs, we use techniques such as pre-setting parts against expected movement, back-step welding and intermittent welds where the drawing allows, and controlled straightening when necessary.
MIG, flux-core, TIG or stick: matching process to part
Most carbon steel production work is done with gas metal arc welding (MIG) because it is fast, clean and well suited to shop conditions. Short-circuit or pulsed modes handle thin material; spray transfer and metal-cored wires put down heavy fillets efficiently on thicker sections.
Flux-cored welding is useful for heavy plate, out-of-position joints and parts that will finish their life outdoors. TIG is chosen for stainless and aluminum, thin material and visible welds where appearance matters. Stick welding rarely appears in production work but remains the tool for field repairs and certain heavy structural joints.
The choice also affects cost. A process that deposits weld metal faster, with less spatter cleanup, lowers unit price over a long run, so we consider it carefully during quoting.
How do repeat orders stay consistent?
Consistency comes from writing things down. Each production part has a traveler that lists the drawing revision, material, weld procedure, sequence, inspection points and finish. Welders work to the procedure for that joint, and the inspection plan defines what gets measured on each part and what gets checked on a sample basis.
Where structural or code requirements apply, procedures follow the governing code, typically AWS D1.1 for structural steel or the applicable standard named in your specification. Weld size and profile are checked with gauges, and dimensional checks are recorded against the drawing.
Material traceability can be maintained by heat number when your quality system requires it, from mill certification through to the finished part.
Traveler with revision, material and procedure
Fixture verification at the start of each run
In-process checks on critical dimensions
Final inspection and records retained with the order
Materials, cutting and finishing
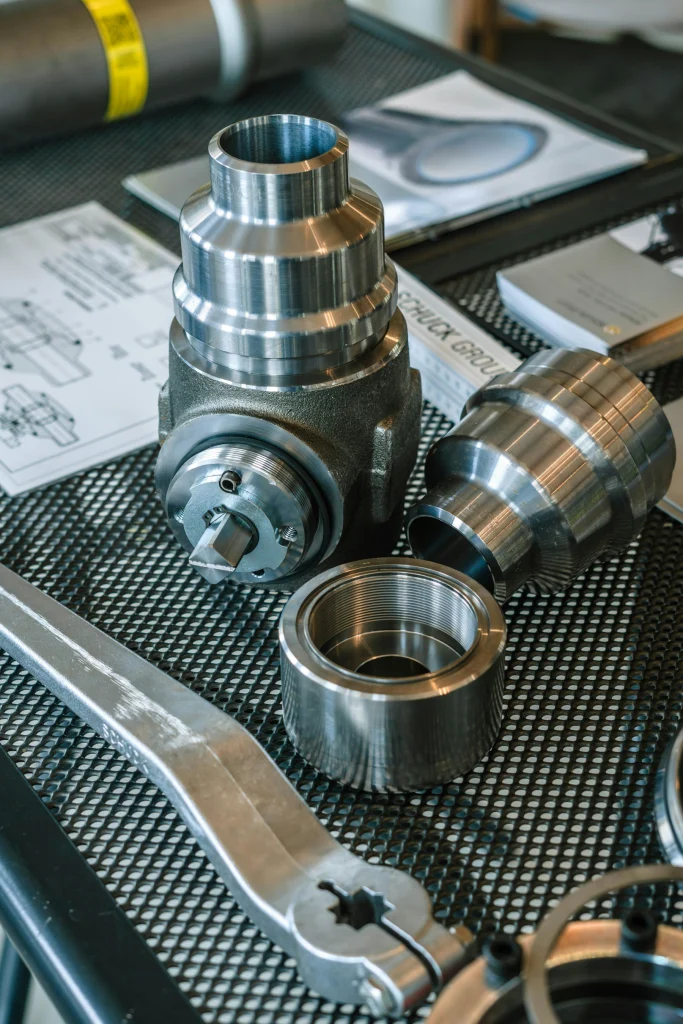
Most production work is carbon steel plate, sheet, tube and structural shapes, with stainless and aluminum for food, chemical, marine and weight-sensitive applications. Parts are cut by saw, plasma or laser, depending on geometry and volume, with laser-cut blanks sourced from qualified suppliers when that is the most accurate and economical route.
Finishing options include grinding and blending welds, shot or abrasive blasting, primer and paint systems, powder coating through finishing partners and hot-dip galvanizing. Stainless parts can be cleaned and passivated after welding to restore corrosion resistance. We confirm finish requirements at the drawing review because they influence how parts are welded and handled.
How a production fabrication job works with Industrial Welding
01
Drawing review
We review drawings for tolerances, weld callouts, materials and finish, and propose changes that make the part easier to build consistently.
02
Fixture and first article
Fixtures are built or set up, a first article is produced and inspected, and the results are sent to you for approval.
03
Production run
Parts are built to the approved revision with travelers, in-process checks and documented weld procedures.
04
Inspect and ship
Final inspection, finishing, labeling and packaging are completed, and records ship with the order or to your quality team.
What affects unit cost in production fabrication?
Unit cost falls as volume rises, mainly because fixture and setup costs are spread across more parts. The biggest variables are part complexity, number of components, weld volume, tolerances, material type and finishing. Drawings with tolerances tighter than necessary, or with welds that require repositioning the part several times, push cost up.
We often suggest small changes that reduce cost without affecting function, such as combining parts, standardizing hole sizes, changing a joint to allow a fillet instead of a groove weld, or adjusting weld lengths. Final approval of any change always rests with your engineering team.
Delivery, packaging and paperwork
Finished parts are labeled, packaged and shipped to your requirements: palletized, crated, bundled or kitted by assembly. Documentation can include inspection records, material certifications and certificates of conformance as your purchase order requires.
Production parts often feed other work we do. Skids and frames support equipment installed by our plant maintenance welding crews, wear liners serve heavy equipment rebuild customers, and support steel is often fabricated alongside industrial structural steel packages. Equipment builders and operators in industrial centers such as Dallas and Midland can receive shipped parts without a local shop visit.
Frequently asked questions
What is the minimum order for production fabrication?
There is no fixed minimum. Short runs of a few identical parts are common, especially for skids and frames. Unit cost improves as volume increases because fixture and setup costs are spread across more parts. Tell us your expected order quantity and annual volume, and we can quote several quantity breaks for comparison.
Can you build parts from our CAD files?
Yes. Send PDF drawings along with native or neutral CAD files such as STEP or DXF. PDF drawings define the requirements, while CAD files help with cut programming and fixture design. If the drawing and model disagree, we raise it before quoting so the controlling document is clear for everyone.
Do you provide first-article inspection?
Yes. A first article is built and inspected against the drawing before the production run, with critical dimensions recorded. You can review the report, inspect the part yourself, or both. The run is released only after approval, and the approved revision becomes the reference for all future orders of that part.
How do you control weld distortion on long frames?
We use fixtures to hold components, plan the weld sequence to balance shrinkage, pre-set parts against expected movement and use intermittent welds where the drawing permits. Measurements are taken during welding as well as at the end. When distortion still exceeds tolerance, controlled straightening brings the part back within limits.
Can you hold parts for scheduled releases?
In many cases, yes. Recurring parts can be produced in economical batches and released against a schedule, which shortens your lead time for each release. Storage terms and quantities are agreed in advance. This arrangement works best with stable drawings and a forecast we can plan material purchases against.
Do you weld stainless and aluminum production parts?
Yes. Stainless and aluminum parts are welded with TIG or pulsed MIG depending on thickness and appearance requirements, using dedicated tools and a separated work area to prevent contamination from carbon steel. Stainless parts can be cleaned and passivated after welding. Aluminum alloy and temper should be specified clearly on the drawing.