When comparing AWS D1.1 vs ASME Section IX, the short answer is that they do different jobs. AWS D1.1 is a complete structural welding code for steel buildings, platforms and supports, covering design, procedures, fabrication and inspection. ASME Section IX only qualifies welding procedures and welders; the pressure code that references it, such as B31.3 or Section VIII, sets everything else.
That difference trips up a lot of buyers. A contractor might say “our welders are ASME certified” when you are buying a structural platform, or “we weld to D1.1” when the job is a process line. Both statements can be true and still miss the point. Below is a practical breakdown of what each document governs, where they line up and how a single plant project often touches both.
Key takeaways
- AWS D1.1 governs welded steel structures. It includes its own acceptance criteria and inspection requirements.
- ASME Section IX is a qualification standard. It does not tell you how much inspection to do or what defects are acceptable; the referencing code does.
- D1.1 permits prequalified welding procedures when all listed conditions are met. Section IX generally requires procedures qualified by test.
- Pressure-boundary welds follow the pressure code; the structure holding up the equipment usually follows D1.1.
- Always confirm the governing code and edition with your engineer of record or authorized inspector before work starts.
What is AWS D1.1?
AWS D1.1, the Structural Welding Code for Steel, is published by the American Welding Society and revised on a regular cycle. It applies to welded structures made from commonly used carbon and low-alloy constructional steels, generally at thicknesses of 1/8 inch and greater. Thinner sheet steel falls under AWS D1.3, stainless structural work under D1.6 and aluminum under D1.2.
D1.1 is unusual because it is self-contained. Within one book it covers:
- Design of welded connections, including weld sizes, effective throats and allowable details for statically and cyclically loaded structures.
- Prequalified welding procedures, with permitted joint geometries, base metal and filler metal combinations and minimum preheat requirements.
- Qualification by test when a procedure falls outside the prequalified limits, along with welder, welding operator and tack welder qualification.
- Fabrication requirements such as fit-up tolerances, weld profiles and repair methods.
- Inspection requirements and acceptance criteria for visual inspection, ultrasonic testing and radiography.
- Stud welding and the strengthening and repair of existing structures.
In a plant, D1.1 is the usual reference for pipe racks, equipment platforms, mezzanines, stair towers, conveyor supports, crane runway components and miscellaneous steel. That is the core of our structural steel work.
What is ASME Section IX?
ASME Boiler and Pressure Vessel Code Section IX is titled Welding, Brazing, and Fusing Qualifications. It establishes how to qualify a welding procedure through testing, how to document it on a procedure qualification record, and how to qualify the welders and welding operators who use it. It classifies base metals by P-Number and filler metals by F-Number and A-Number, so a single qualification test can cover a family of similar materials.
What Section IX does not do is just as important. It does not say how big a weld should be, how much radiography a joint needs, whether a bit of porosity is acceptable or when post-weld heat treatment is mandatory. Those rules live in the referencing codes, including:
- ASME B31.3 for process piping in refineries, chemical plants and similar facilities.
- ASME B31.1 for power piping.
- ASME Section VIII for pressure vessels and Section I for power boilers.
- API 650 and API 653 for welded storage tanks, which reference Section IX for procedure and welder qualification.
So when someone says a weld is “to Section IX”, the right follow-up is “under which construction code?”
How do AWS D1.1 and ASME Section IX differ on procedure qualification?
This is where the two documents split most clearly. Under D1.1, a WPS can be prequalified. If the contractor uses a listed steel, a matching filler metal, a joint geometry from the prequalified figures, the required minimum preheat and a permitted process, the WPS can be written and used without welding and testing a coupon first. That makes routine structural work fast to set up.
Under Section IX, procedures are generally qualified by test. The contractor welds a coupon, a lab performs tension and bend tests and, where toughness is required, impact tests, and the results are documented on a PQR. The WPS then cites that PQR. Section IX does allow adoption of certain AWS standard welding procedure specifications under defined conditions, but the default expectation is a tested procedure owned by the organization doing the welding.
Variables are organized differently
Both documents control the same physical variables: process, base metal, filler, thickness, position, preheat, heat treatment, gas and electrical settings. They just organize and limit them differently. D1.1 uses its own tables and base metal groups, while Section IX uses P-Numbers, essential and nonessential variables, and supplementary essential variables that apply when notch toughness is required. A PQR written to one document is not automatically valid under the other. Our guide to WPS and PQR documents explains how those records fit together.
Welder qualification under each code
Both documents require each welder to pass a performance test that qualifies them for certain processes, positions, thicknesses and, for pipe, diameters. Test coupons are typically evaluated by bend testing, and both allow radiographic examination of the test weld in many situations. Both also include a continuity rule: a welder who has not used a process for about six months typically loses that qualification unless continuity is documented.
The practical differences show up in the details. Position designations, diameter ranges, and how a pipe test qualifies a welder for plate (and vice versa) are handled differently. A welder who holds a 6G pipe qualification under Section IX is often highly capable on structural work too, but the D1.1 qualification still has to be documented under D1.1 rules, or accepted under the provisions D1.1 provides. Ask the contractor to show qualifications under the code that actually governs your joint.
Tack welders and welding operators
D1.1 recognizes tack welders as a separate qualification category, which matters because tack welds often become part of the final weld. Both documents also distinguish manual welders from welding operators who run mechanized or automatic equipment, such as orbital pipe welders or submerged arc tractors. If your job involves automated welding, check that the operators, not just the hand welders, hold the right qualifications.
Why the code edition matters
Both AWS and ASME revise their documents on a regular cycle, and clause numbers, tables and some technical requirements change between editions. A procedure qualified years ago may still be valid, but the contract should state which edition governs new work. Owners occasionally discover mid-project that their specification references an outdated edition while the contractor’s procedures follow a newer one. Settling the edition question at bid time avoids arguments about acceptance criteria later.
Inspection and acceptance criteria
D1.1 contains its own inspection chapter. It defines visual acceptance criteria for cracks, fusion, undercut, porosity and weld profile, and it includes acceptance criteria for ultrasonic and radiographic examination, with different limits for statically and cyclically loaded connections. The Inspector role is often filled by an AWS Certified Welding Inspector, though the contract documents define who qualifies.
Under ASME-referenced work, Section IX is silent on production inspection. The construction code decides. B31.3, for instance, sets required examination by fluid service category; for normal fluid service it typically calls for random examination of a small percentage of circumferential butt welds, with more for severe cyclic conditions. Section VIII ties the extent of radiography to the joint efficiency used in the vessel design. Third-party roles differ too: stamped boilers and vessels involve an Authorized Inspector from an authorized inspection agency, while process piping relies on the owner’s inspector. For a closer look at the techniques themselves, read our overview of weld inspection methods.
Where both codes meet on one project
Real plant jobs rarely stay inside one code. Consider a typical unit tie-in during a turnaround:
- The new pipe rack extension and access platform are designed and fabricated under AWS D1.1.
- The process piping on that rack is built under ASME B31.3, with welding procedures and welders qualified to Section IX.
- Pipe shoes and trunnions welded directly to the pipe are attachments to the pressure boundary, so those welds follow the piping code and its qualified procedures, even though they look like structural welds.
- A new nozzle on an existing pressure vessel falls under the vessel’s construction code and, for repairs or alterations, the jurisdiction’s rules, which often reference the National Board Inspection Code.
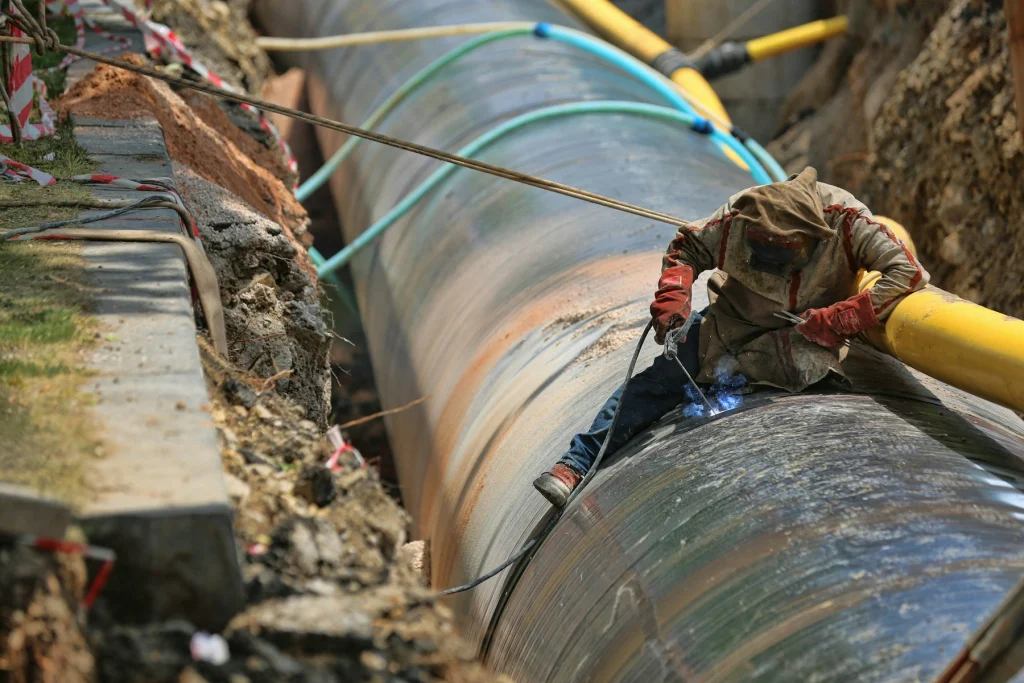
The boundaries matter. A support clip welded to a pipe with a D1.1 prequalified structural WPS may be perfectly sound and still be noncompliant, because the weld touches the pressure boundary. Good contractors flag those boundaries during estimating. Our pipe welding crews and structural crews work from a shared weld map for exactly that reason.
A note on tanks and vessels
Repairs to code-stamped boilers and pressure vessels usually require an organization holding the appropriate repair authorization recognized by the jurisdiction, along with an inspector’s involvement. Many tank and hopper jobs, such as brackets on non-pressure equipment, ladders, platforms and wear liners, do not fall under those rules. Knowing which side of that line your job sits on keeps the scope honest. Our tanks and vessels repair page explains the non-code work we take on and when an authorized repair organization is required.
Which code applies to your job? A quick decision guide
Start with what the weld does and what it holds:
- Does the weld contain pressure or process fluid? If yes, a pressure code applies (B31.3, B31.1, Section VIII, Section I, API 650/653 or API 1104 for pipelines), and qualification usually follows Section IX or the code’s own rules.
- Is it welded directly to a pressure-containing part? If yes, treat it as part of the pressure scope even if its purpose is structural.
- Is it a building or support structure in carbon or low-alloy steel? AWS D1.1 is the usual reference, unless the engineer specifies another code such as a bridge or seismic supplement.
- Is it thin sheet, stainless or aluminum structural work? Check whether D1.3, D1.6 or D1.2 is specified instead of D1.1.
- Is it non-code fabrication? Owners often still specify D1.1 workmanship as a baseline. Write that into the purchase order rather than assuming it.
When in doubt, the engineer of record, authorized inspector or your insurer’s representative has the final word. Local jurisdictions in places such as Houston also have their own boiler and pressure vessel requirements, so confirm with the authority having jurisdiction.
Checklist for specifying welding code requirements
- Name the governing code and edition for each part of the scope in the purchase order or bid package.
- Mark pressure-boundary versus structural welds on the drawings or weld map.
- State whether D1.1 prequalified WPSs are acceptable or whether you require qualified-by-test procedures.
- Require WPSs, PQRs and welder qualifications for review before mobilization.
- Define the inspection extent, method and acceptance criteria, or reference the code clause that does.
- Identify who performs inspection: contractor quality staff, a third-party CWI, NDE technicians or an authorized inspector.
- Specify material certification and traceability requirements.
- List required deliverables at handover, such as weld maps, NDE reports, PWHT charts and a data book.
Frequently asked questions
Is ASME Section IX stricter than AWS D1.1?
Not exactly. They address different things. Section IX generally requires procedures to be qualified by test, which is more demanding up front than D1.1 prequalification. But D1.1 includes design, fabrication and inspection acceptance criteria that Section IX leaves to other codes. The overall rigor of a pressure job depends on the construction code, not Section IX alone.
Can a welder qualified under ASME weld structural steel?
Physically, yes, and many pipe welders are excellent structural welders. On paper, the welder needs a qualification that satisfies the code governing the structure. For D1.1 work, that typically means a D1.1 qualification test or documentation accepted under D1.1 provisions. Ask your contractor to show the qualification that matches the code on your drawings.
Does D1.1 apply to pipe supports?
D1.1 often governs the steel framing of pipe supports and racks. Any weld made directly to the pipe itself, such as a shoe, trunnion or lug, is usually considered part of the piping system and follows the piping code with Section IX qualified procedures. The engineer of record should define that boundary on the drawings.
What is the difference between a CWI and an Authorized Inspector?
A Certified Welding Inspector holds an AWS certification covering welding inspection knowledge and is commonly used for structural and general fabrication work. An Authorized Inspector is employed by an authorized inspection agency and commissioned to inspect ASME-stamped boilers and pressure vessels. They are different credentials for different regulatory roles, and some projects need both.
Do these codes apply to non-code repair work?
Not automatically. If equipment is not built or stamped to a code, the owner decides what standard to apply. Many plants still require D1.1 workmanship or Section IX qualified procedures as an internal standard, because it gives a documented, repeatable baseline. Put that requirement in writing so every bidder prices the same thing.
Working with a contractor who reads the codes
Choosing between AWS D1.1 and ASME Section IX is rarely a choice at all. The equipment and its service decide, and a capable contractor helps you draw the lines clearly before the first arc is struck. When you send a project to Industrial Welding, include the governing codes and drawings if you have them, and we will identify the procedures, qualifications and inspection steps your scope requires. Request a free written quote through the Get a Quote form and we will respond with an itemized scope.